Speed Settings
The settings that took the machine from about 46 s per part (first run, 11-14) to about 7 s
(~511 parts per hour, 11-18). All are in Software/pnpvision/config.toml unless noted.
| Setting | Value | What it does | Notes |
|---|---|---|---|
| streamed moves | on (in code) | sends a whole pick-inspect-place sequence to Klipper at once instead of waiting after every move | the biggest single gain |
[run] xy_feedrate |
24000 mm/min | X/Y travel during jobs (400 mm/s) | printer.cfg allows 600 mm/s |
[run] accel |
5000 mm/s² | acceleration during jobs, restored afterwards | printer.cfg max 7500 |
[run] z_feeds |
approach/lift/inspect 3000, touch/release_lift 1500 mm/min | Z speeds per phase | Z is capped at 50 mm/s in printer.cfg |
[run] vac_ms / release_ms |
150 / 200 ms | wait for vacuum before lifting / for release before lifting | lower risks dropping parts |
[run] verify |
false | skip the empty-nozzle check after placing | saves ~8 s per part; board-check covers it afterwards |
[lighting.up] settle_s |
0.10 s | wait after the ring light before the inspection photo | |
rotation (printer.cfg [manual_stepper stepper_r]) |
360 °/s, 3000 °/s² | nozzle turn speed | |
feeder stroke (pnp_feeders.cfg) |
400 ms out / 400 ms back | faster or ramped strokes bounced parts out |
Where the time goes now
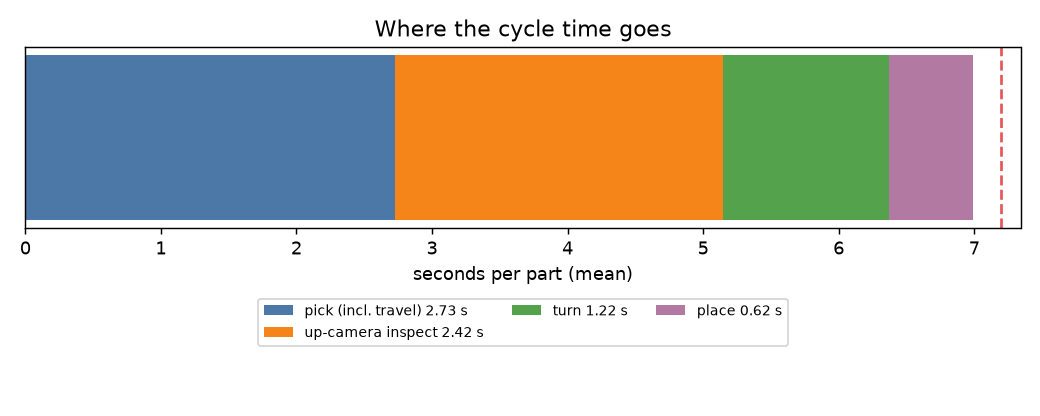
Pick including travel ~2.7 s, up-camera inspection ~2.4 s, turn ~1.2 s, place ~0.6 s. Next candidates: overlapping the feeder stroke with motion, and pre-turning the nozzle on the way to the up camera.
Change one thing at a time
After each change run the 23-part test job and check-board: a faster setting that costs
picks or accuracy is not a gain. If Z starts to skip (clicks, wrong heights), go back:
Troubleshooting.